Alloy Steel CNC Machining Service
Plyconn machines alloy steel components from prototype through production, coordinating stock condition, heat treatment, hard machining, grinding, surface protection, and dimensional inspection.
- Material-specific DFM and process selection
- Critical features down to ±0.01 mm after review
- Machining, secondary processing, and inspection
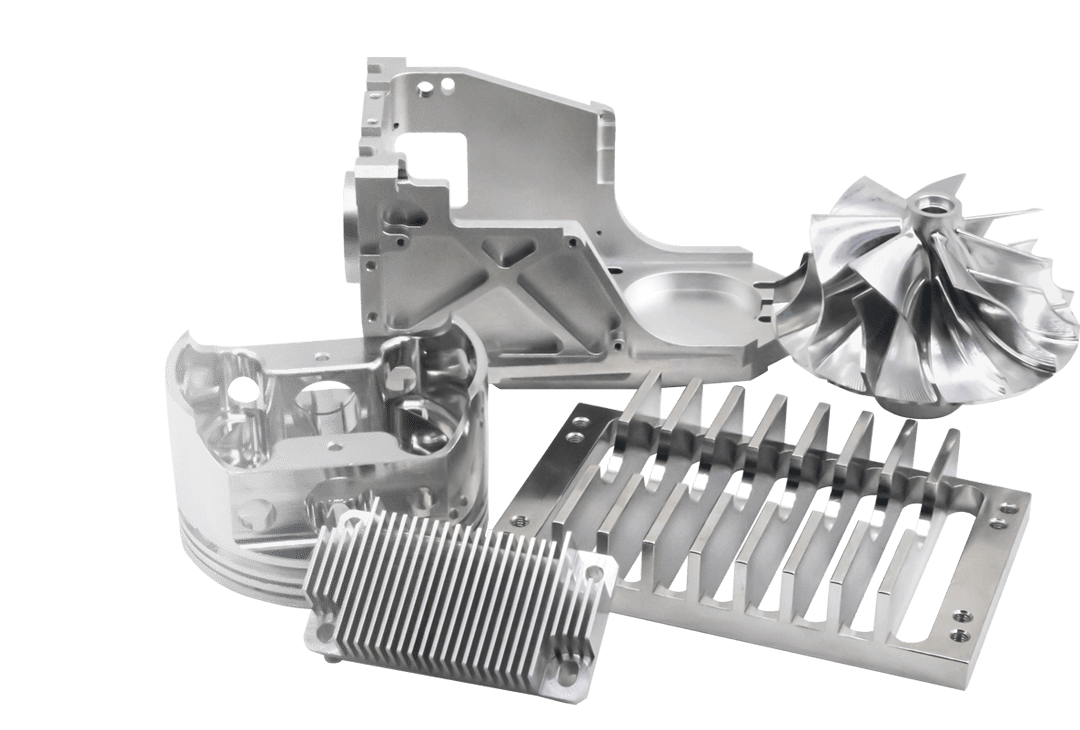
Alloy Steel CNC Machining Capabilities
Practical starting points; final capability depends on grade, condition, part size, geometry, finishing, and inspection method.
Why Use Alloy Steel for CNC Machining?
Material selection connects mechanical performance, service environment, manufacturability, finishing, availability, and total production cost.
High strength
Alloy additions and heat treatment provide strength for shafts, gears, tools, and loaded structures.
Wear resistance
Carburizing, nitriding, through hardening, and coatings support sliding and contact surfaces.
Toughness options
Grade and temper can balance impact strength, fatigue resistance, and hardness.
Heat-treatment response
Material condition can be tailored for machining first and performance after hardening.
Broad availability
Common bar, plate, forging, and tubing forms support prototype and repeat production.
Finish compatibility
Grinding, black oxide, plating, phosphate, nitriding, and PVD are widely available.
CNC Machining Services for Alloy Steel Parts
We select the platform around geometry, datum relationships, access, size, batch volume, and manufacturing risk.
5-Axis CNC Machining
Complex housings, deep cavities, compound angles, and multi-face geometry tied to a common datum.
Explore service →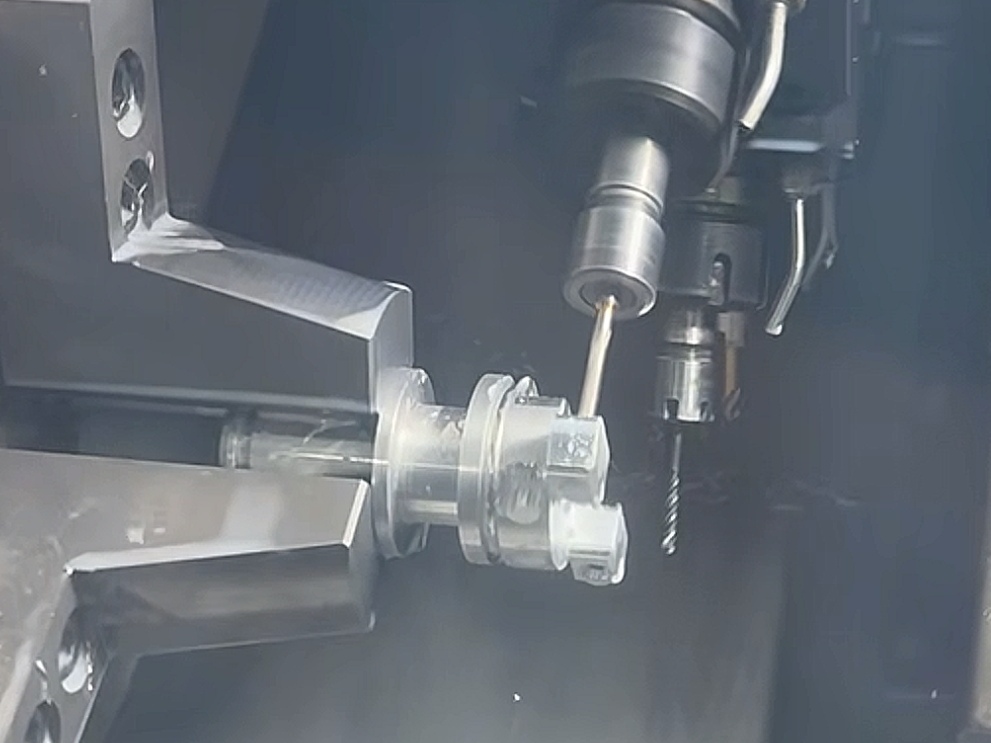
Mill-Turn Machining
Rotational parts with flats, cross holes, pockets, threads, and back-working in one coordinated cycle.
Explore service →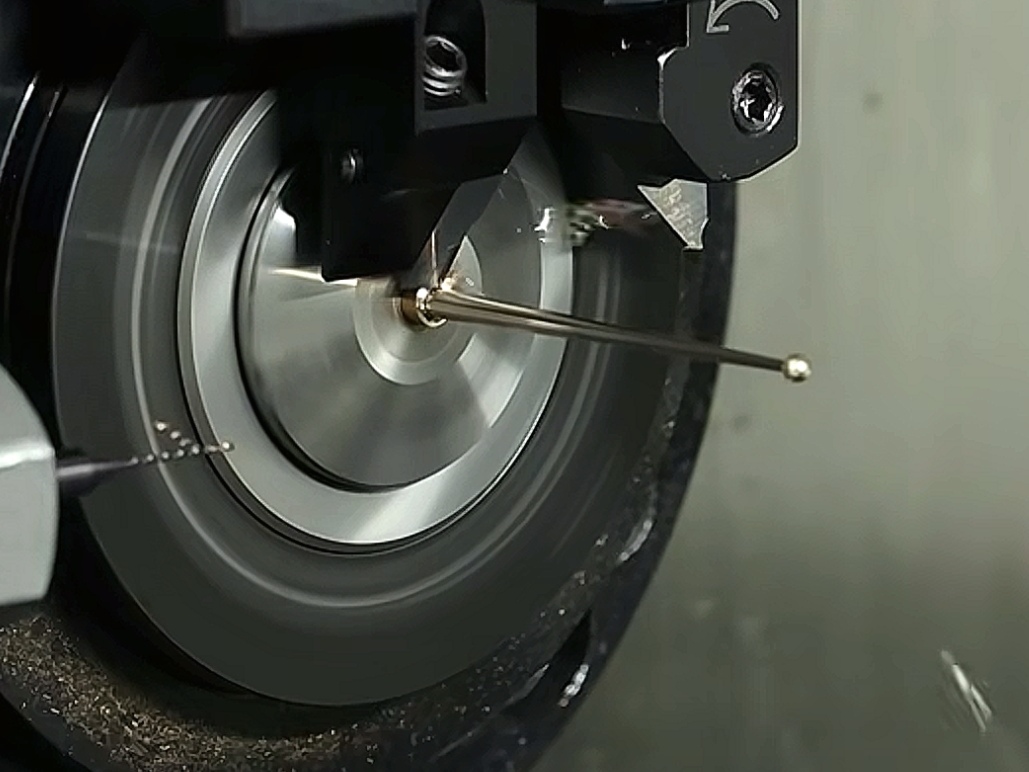
Swiss Machining
Small-diameter fittings, pins, inserts, connectors, and high-volume turned components.
Explore service →
Electrical Discharge Machining
Conductive hard materials and features that are inaccessible to conventional cutters.
Explore service →Alloy Steel Grades for CNC Machining
International references are consolidated for sourcing comparison. Nominal equivalents can differ by chemistry, product form, condition, and governing standard.
| Grade | International cross-reference | Machining performance / behavior | Suitable applications |
|---|---|---|---|
| 4140 / 42CrMo4 | AISI 4140 · EN 1.7225 / 42CrMo4 · GB 42CrMo · JIS SCM440 | Good machinability in annealed or prehard condition; stable heat-treatment planning is important. | Shafts, fixtures, spindles, gears, and structural parts |
| 4340 / 34CrNiMo6 | AISI 4340 · EN 1.6582 / 34CrNiMo6 · GB 40CrNiMoA · JIS SNCM439 | High strength and toughness; cutting becomes demanding as hardness rises. | Aerospace shafts, highly loaded gears, and fasteners |
| 8620 | AISI 8620 · EN 1.6523 / 20NiCrMo2-2 · GB 20CrNiMo · JIS SNCM220 | Machines well before carburizing; finish stock must account for heat-treatment movement. | Case-hardened gears, pins, bushings, and wear components |
| 52100 | AISI 52100 · EN 1.3505 / 100Cr6 · GB GCr15 · JIS SUJ2 | Often rough machined soft, hardened, then ground or hard turned. | Bearings, races, rollers, gauges, and precision wear parts |
| D2 / SKD11 | AISI D2 · EN 1.2379 / X153CrMoV12 · GB Cr12Mo1V1 · JIS SKD11 | High wear resistance; EDM and grinding commonly complete features after hardening. | Dies, punches, inserts, and cutting tools |
** Specify the governing standard, condition, product form, and certificate requirement. We verify equivalency before production.
Alloy Steel CNC Machining Tolerances and Part Sizes
Critical dimensions are reviewed against material condition, wall thickness, datums, tool access, temperature, and inspection method.
| Capability | Reference value | Application note |
|---|---|---|
| Typical tolerance | ±0.025 mm | For controlled drawing dimensions |
| Precision features | ±0.01 mm | Subject to geometry and inspection review |
| Surface finish | Ra 0.8 μm | Achievable on accessible machined surfaces |
| 5-axis envelope | 600 × 600 × 500 mm | Complex multi-face components |
| 3-axis travel | 1,000 × 600 × 600 mm | Plates, housings, and fixtures |
| Turning range | Ø3–300 mm | Pins, fittings, shafts, and sleeves |
| Geometric tolerance | ⏥ 0.02 mm | Typical position Ø0.03–0.05 mm |
| General tolerance | ISO 2768-mK | Unless the drawing specifies otherwise |
Surface Finishes for Alloy Steel CNC Machined Parts
Choose a finish by function first. Thickness, masking, and final dimensions are defined before machining where tolerances are affected.
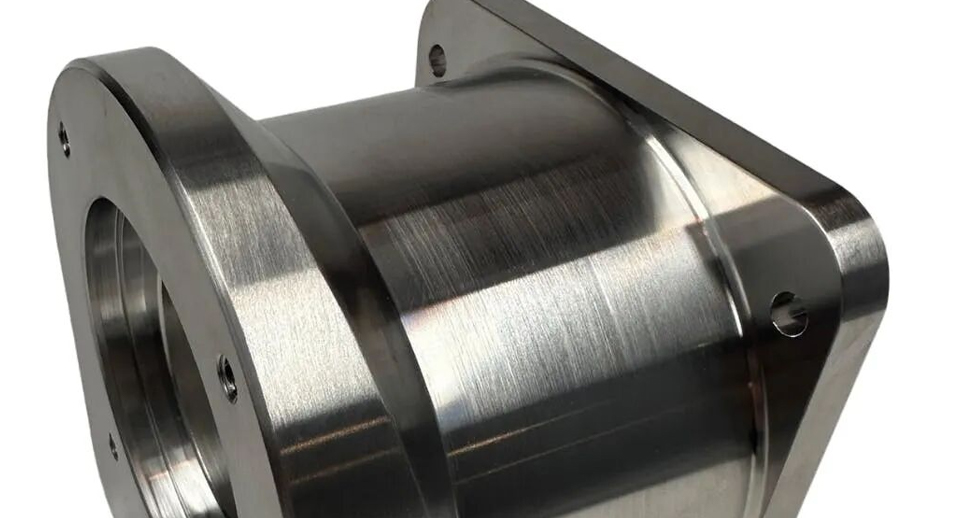
As machined
Functional finish before protection or heat treatment.
No buildup. Deburring can affect small edges.
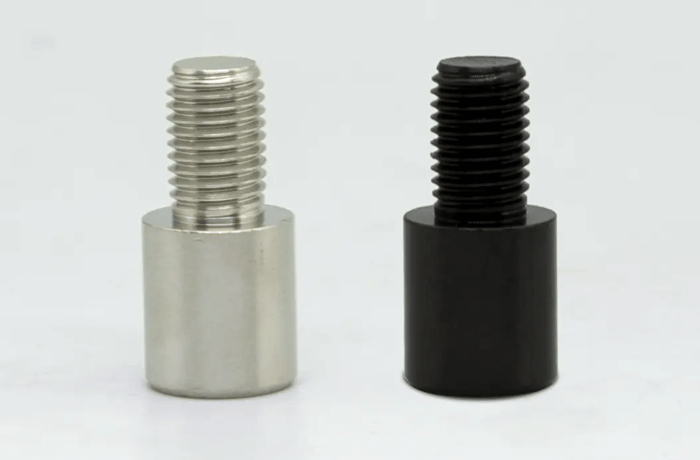
Black oxide
Dark conversion finish with light corrosion protection.
Minimal. Negligible dimensional change.
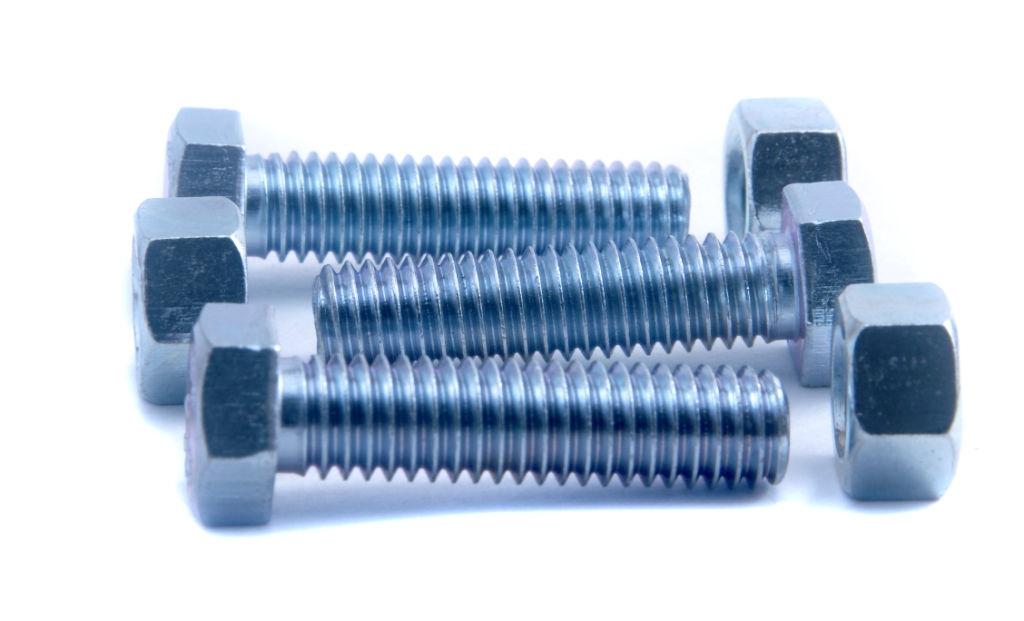
Zinc plating
Economical corrosion protection.
Allow for buildup. Mask threads and precision fits as required.
Electroless nickel
Uniform corrosion and wear protection.
Allow for buildup. Include deposit thickness in final dimensions.
Phosphate coating
Oil-retaining conversion finish for wear and corrosion.
Minimal. Small but process-dependent dimensional effect.
PVD coating
Thin hard coating for wear tools and sliding parts.
Allow for buildup. Usually several micrometers.
Heat Treatment and Finish Machining in Alloy Steel CNC Machining
Hardness, case depth, toughness, distortion, and final geometry are planned as one manufacturing route.
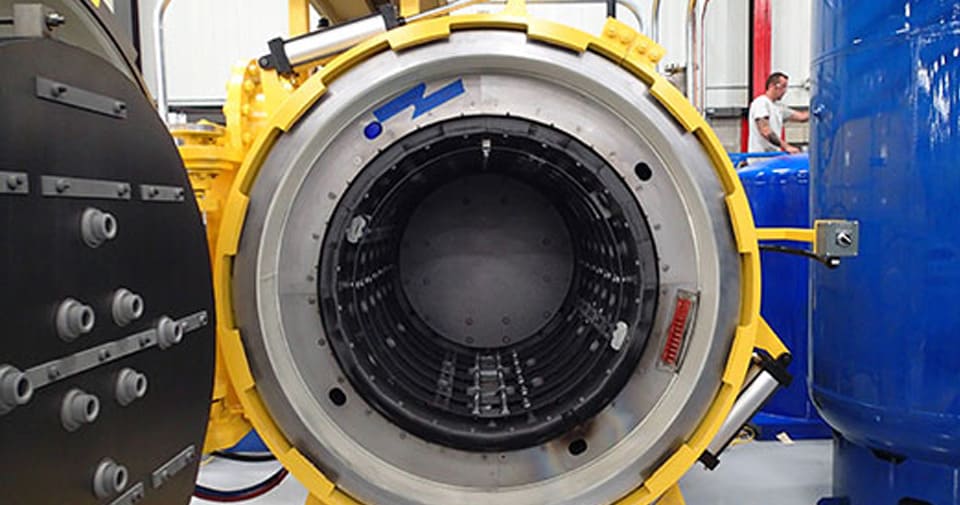
Quench and temper
Sets bulk hardness and toughness for shafts, tooling, and structural components.
Carburizing and nitriding
Creates a hard wear-resistant case while retaining a tougher core.
Stress relieving
Can reduce residual stress before final machining or grinding.
Grinding after heat treatment
Restores size, roundness, flatness, runout, and surface finish after hardening.
Alloy Steel CNC Machining Project Examples
Examples of material selection, process planning, finishing, and inspection for common component types.
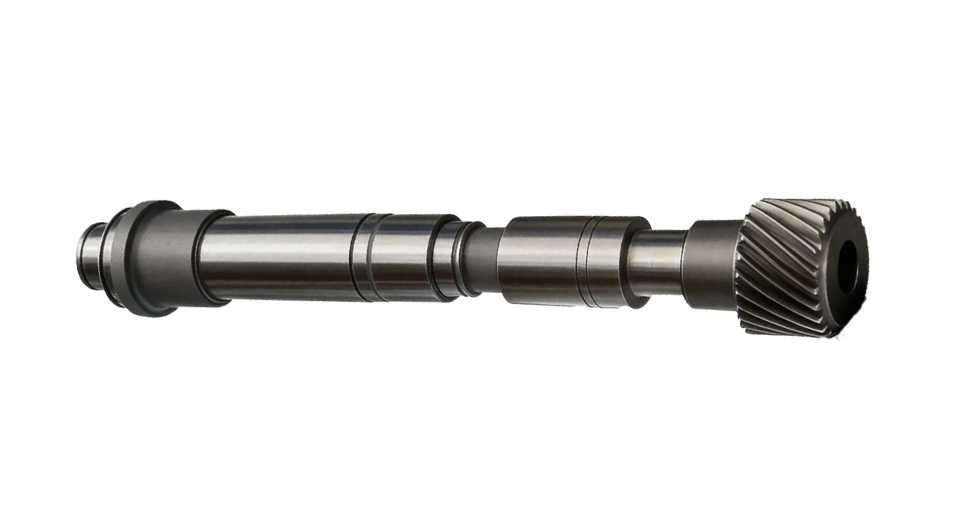
Drive Shaft
- Grade
- 4140
- Process
- Mill-turn, heat treatment, grinding
Bearing seats, splines, and runout controlled through the final hardened condition.
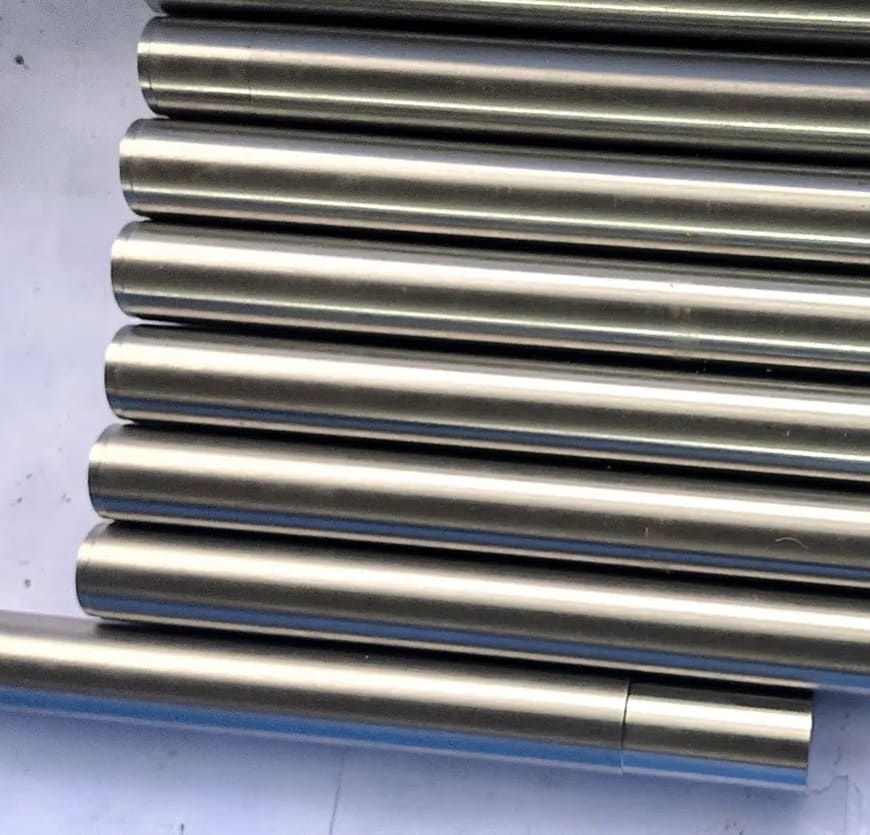
Case-Hardened Gear Blank
- Grade
- 8620
- Process
- Turning, carburizing, finish grinding
Wear surface and tough core combined with controlled bore and face geometry.
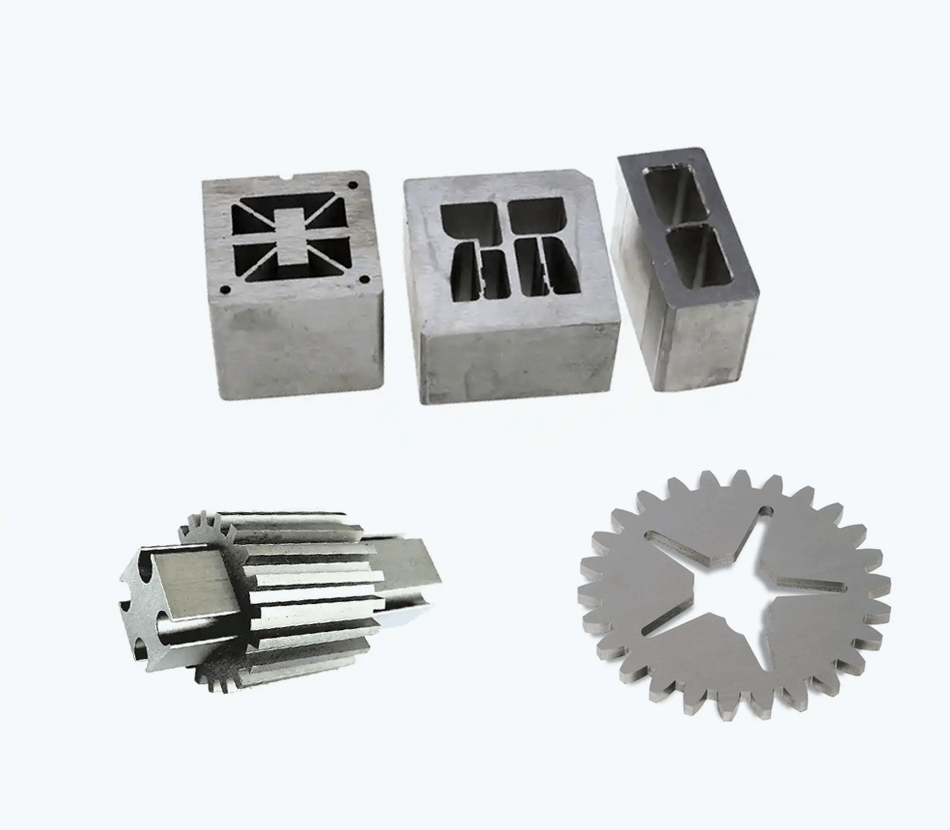
Tooling Insert
- Grade
- D2
- Process
- Milling, hardening, EDM, grinding
Sharp detail and wear resistance completed after heat treatment.
Quality Control for Alloy Steel CNC Machined Parts
Inspection is planned from the drawing. We identify datum access, measurement uncertainty, finishing state, sampling frequency, and required records before production.
Learn about our quality systemIncoming material control
Grade, condition, product form, heat or lot identity, and requested mill certificates are checked before release.
First article inspection
Critical dimensions, datums, threads, surface finish, and visual requirements are verified before batch production.
In-process verification
Machine probing, calibrated gauges, and scheduled checks monitor tool wear and dimensional drift.
Final dimensional inspection
CMM, optical, contour, roughness, thread, and conventional measurement are selected around drawing risk.
Available documentation
FAI, dimensional, CMM, material, finish, heat-treatment, and conformity records are available by requirement.
Repeat-order control
Approved programs, fixtures, inspection plans, revisions, and traceability records support consistent repeat production.
Our Alloy Steel CNC Machining Workflow
A clear workflow carries the project through engineering review, production, secondary processing, inspection, and shipment.
Upload files
Send CAD, drawing, material condition, quantity, finish, tolerances, and documentation needs.
Quote and manufacturability analysis
We review geometry, stock, tooling, distortion, datums, finishing allowance, inspection, lead time, and cost.
Machining and first article inspection
Material is released, setups are controlled, and the first part is inspected before the remaining quantity proceeds.
Heat treatment and post-processing
Approved thermal processing, deburring, finishing, marking, and cleaning are coordinated.
Final inspection and shipping
Dimensions, finish, appearance, documents, cleaning, and packaging are verified before shipment.
Alloy Steel CNC Machining FAQs
Should alloy steel be machined before or after heat treatment?
Most stock is rough machined before heat treatment and finish machined, ground, or EDM processed afterward.
Can you machine prehardened 4140?
Yes. Tooling and parameters are selected for the supplied hardness and required finish.
How is heat-treatment distortion controlled?
We use stock allowance, balanced machining, stress relief, stable fixturing, and post-treatment finishing.
Discuss Your Alloy Steel CNC Machining Project
Send us your drawing, material, quantity, and quality requirements.
We’ll help define the next step.